It is 3 AM in the Guangzhou industrial district. The air filtration system hums at 45 decibels, masking the sound of the timing machines. A QC technician wearing anti-static gloves picks up a Breitling Navitimer replica. He does not look for perfection; he looks for survivability. In 2026, the question is not whether the watch is flawless—it is whether the flaw is within the margin of error that keeps the dealer from demanding a refund. Similar to the original single myth narratives, this is the black box of factory inspection.
The Black Box: Inside the 2026 QC Facility
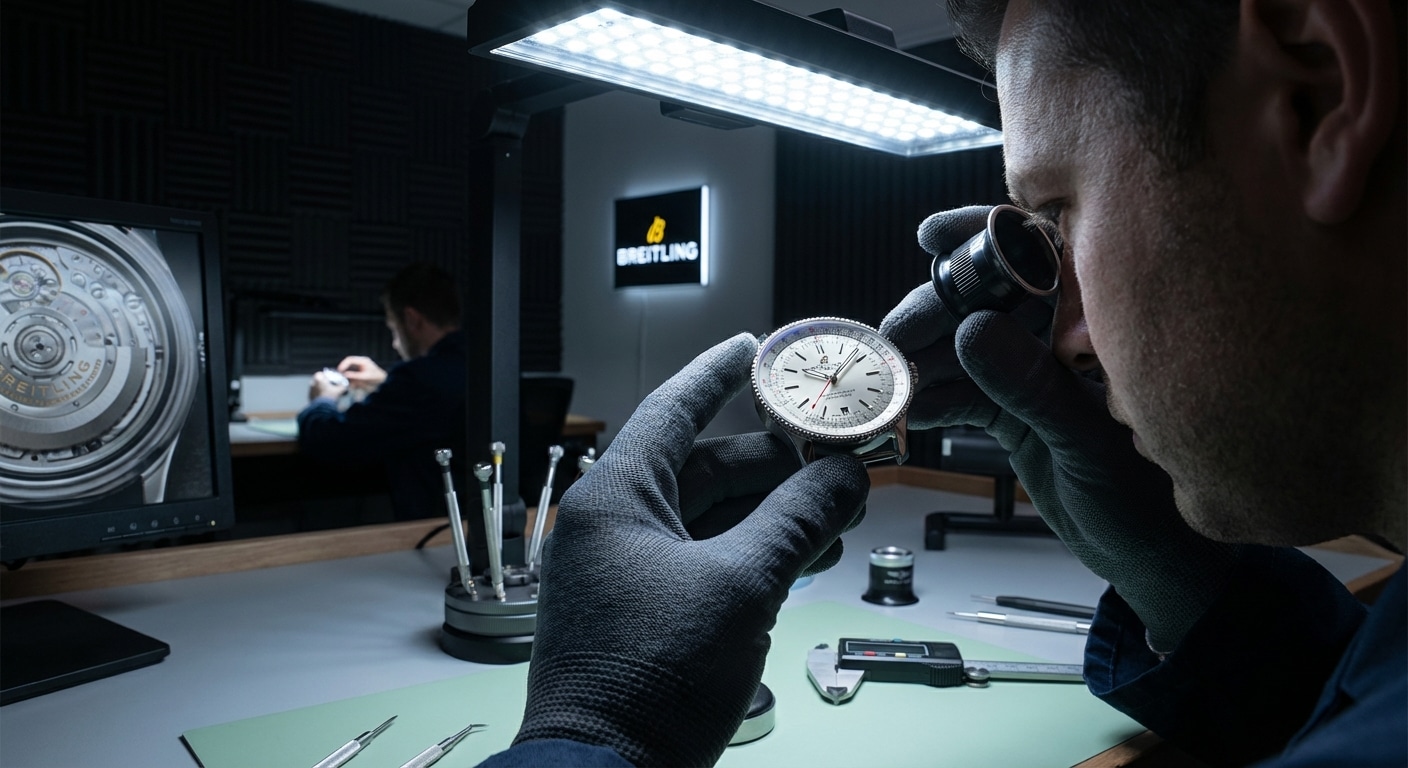
Access to a top-tier QC room in 2026 is restricted not by security clearance but by operational secrecy. The physical layout is designed to eliminate variables that could mask defects during the final assessment. In facilities operated by Clean factory and VS factory, the environment is controlled with surgical precision to ensure consistency across batches. This is not merely about cleanliness; it is about creating a standardized baseline where any deviation becomes immediately visible to the human eye.
Environmental Controls and Lighting Standards
Inspection rooms now utilize 5000K-6000K daylight LEDs calibrated to an intensity of 1000 lux. This specific color temperature and brightness level are chosen to reveal dust particles and luster inconsistencies that warmer or dimmer lighting would hide. The air pressure within these rooms is maintained at a positive level to prevent dust from settling on the movement during the final casing process. A single speck of dust on the dial or movement bridge can trigger a rejection, so the air filtration system runs continuously to maintain ISO standards.
The Human Factor: Technician Shifts and Fatigue
Despite automation, the final judgment call remains human. QC staff work 4-hour rotating shifts to maintain visual acuity, as error rates increase by 15% after hour 3 of continuous inspection. This biological limitation dictates the throughput cap of approximately 200 units per technician daily. Factories prioritize speed, but pushing beyond this limit risks letting defects slip through due to eye fatigue. The human element remains the weakest link in the chain, which is why shift rotation is strictly enforced.
Digital Tracking and Batch Logging
Every unit is scanned into a local ERP system with a timestamp upon entering the QC zone. This data is not shared with buyers but is used internally to track technician performance and identify failure clusters. If a specific batch shows a high rejection rate, management can trace it back to the specific shift or technician responsible. This digital trail ensures accountability within the factory, even if it remains invisible to the end consumer.
Expert Authentication Insight
Request timestamped QC photos from the dealer before shipment. If the lighting color temperature varies wildly between photos or dust is visible on the movement bridge, the inspection environment was substandard. Consistent lighting and cleanliness in the photos are proxies for the actual QC conditions.
Timekeeping Tolerances: The +/- Seconds Debate
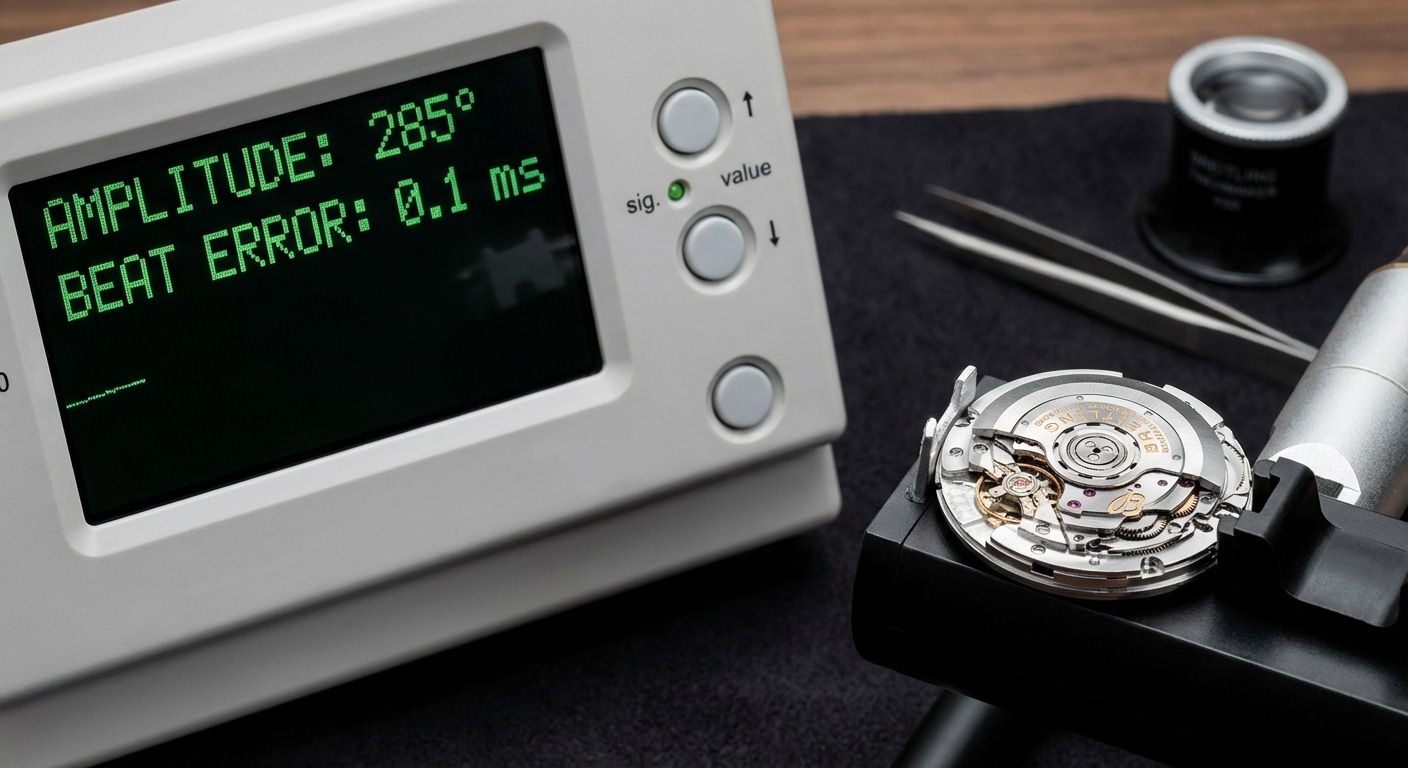
The numbers on a timegrapher are the closest thing to an objective truth in the replica industry, yet they are often misunderstood by buyers. Factories define pass rates based on static measurements that may not reflect real-world performance. Understanding the gap between machine readings and wrist behavior is critical for evaluating the actual quality of the movement inside.
Static vs. Dynamic Timing Results
Timing machines measure static positions such as dial up or crown down. A watch passing at -5s/day static may run +10s/day on wrist due to dynamic amplitude loss caused by movement and gravity. Factories prioritize static pass rates because they are easier to control and document. The dynamic performance depends on how the watch is worn, which is outside the factory’s control sphere.
Amplitude and Beat Error Thresholds
Minimum amplitude acceptance is set at 270 degrees for a unit to pass initial inspection. Beat error must be under 0.5ms to ensure the balance wheel is swinging evenly. Units falling below these thresholds are sent for regulation rather than scrap, unless the movement itself is defective. This distinction saves material costs while maintaining functional standards.
The 2026 Standard Shift
In 2026, Clean factory tightened tolerance from +/- 15s/day to +/- 10s/day to compete with VS factory market positioning. However, this stricter standard is only enforced on premium batches designated for direct high-value orders, not on general stock inventory. Buyers purchasing from general stock may still receive units within the older, looser tolerance range.
Expert Authentication Insight
Use a timegrapher app immediately upon receipt of the watch. If amplitude is below 250 degrees within the first 24 hours, the movement was likely not fully wound or regulated during factory QC. Low amplitude out of the box indicates a lack of final regulation before casing.
Cosmetic Grading: Microns and Light Angles
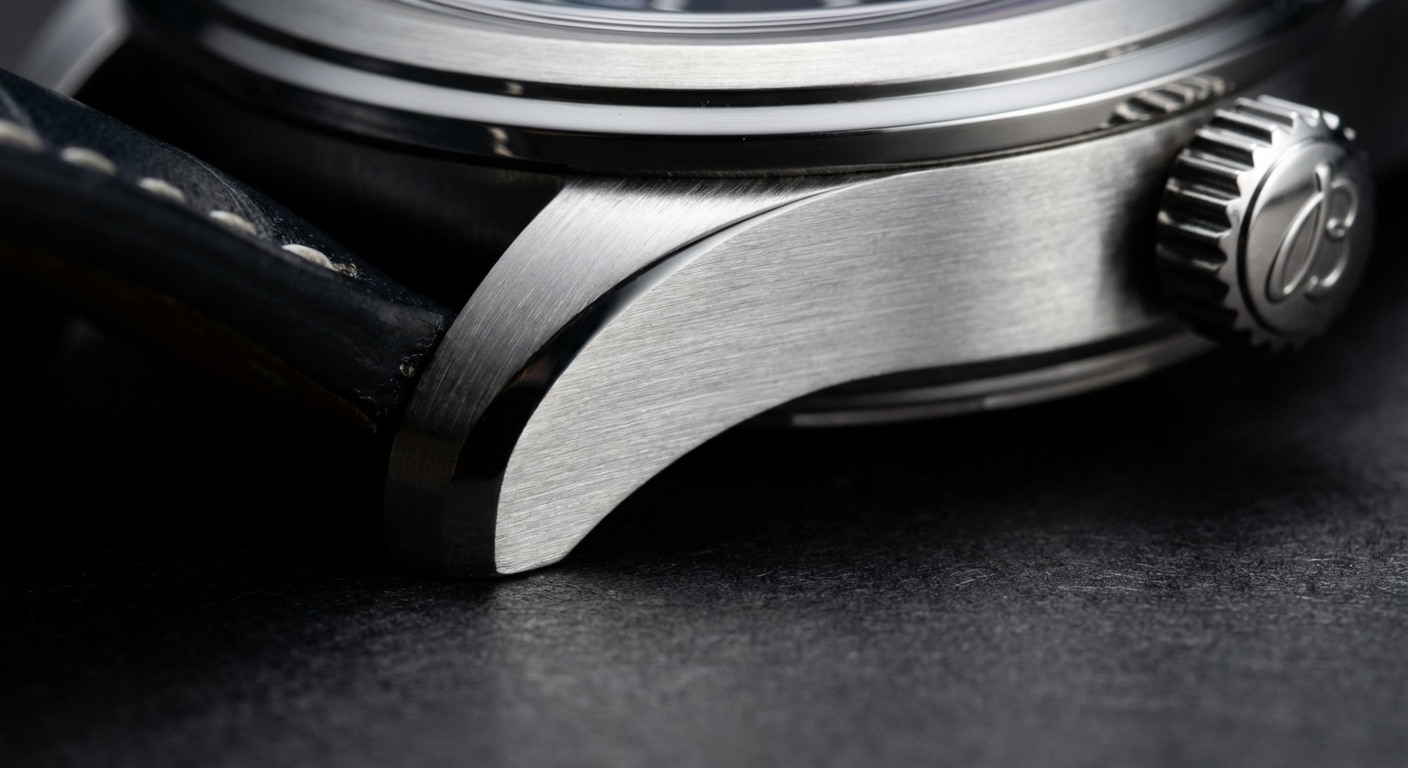
Visual flaws are subjective, but factory management quantifies them to streamline the approval process. What a collector sees as a defect, a factory sees as an acceptable variance within tolerance. The goal is to maximize yield without triggering dealer returns, so the definition of passable is constantly adjusted based on market feedback.
Polishing and Brushing Consistency
Brushing grain must align within 5 degrees across lugs to maintain visual continuity. Polishing marks under 0.1mm length on case sides are considered passable if not visible from 30cm. This distance rule allows minor surface imperfections to exist as long as they do not detract from the wrist presence. Factories accept that perfect polishing is economically unviable at this price point.
Bezel Alignment Tolerances
Maximum allowable misalignment is 0.5mm at the 12 o’clock marker. Anything exceeding this threshold is sent for rework rather than scrapped. In 2026, the introduction of laser alignment tools reduced this error rate by 40%, but human assembly still introduces variance. The bezel remains one of the most common points of failure in cosmetic inspection.
Crystal and AR Coating Inspection
Dust under the crystal is an automatic fail regardless of size. AR coating scratches are passable only if under 2mm and located on the edge, not the center viewing zone. Central scratches interfere with legibility and are grounds for rejection. Edge scratches are deemed acceptable as they do not impact the primary function of the watch.
Expert Authentication Insight
Use a 10x loupe under a single point light source and rotate the watch 360 degrees. If polishing waves are visible on the flat lug surfaces, the QC ignored surface topology standards. Consistent flatness indicates proper finishing; waves indicate rushed polishing.
Automation vs. Human Eye: Clean/VS Upgrades
The narrative that top-tier factories rely solely on magnifying loupes and experienced eyes is outdated. In 2026, the divide between acceptable and rejectable units is increasingly defined by software algorithms and optical sensors. Clean factory and VS factory have led this transition, integrating automated optical scanning into their final assembly lines. This shift does not eliminate human involvement, but it changes the human role from primary detector to exception handler. The goal is consistency at scale, removing the variance introduced by technician fatigue or subjective judgment.
Optical Scanning for Case Dimensions
Manual calipers introduce human error through pressure variance and reading angles. The new 2026 production lines utilize non-contact laser calipers positioned at three critical points along the case profile. These systems verify case thickness within a 0.05mm tolerance. This precision is crucial for catching casting shrinkage errors that occur during the cooling phase of steel manufacturing. A human inspector might miss a 0.1mm deviation on a curved lug surface, but the laser map flags it immediately. This technology ensures that case dimensions remain consistent across batches, preventing the fitment issues often seen when swapping bracelets between units of the same model.
Automated Pressure Testing
Water resistance testing has historically been a bottleneck prone to inconsistency. Manual pumps rely on the operator to maintain pressure steady for the required duration. The updated facilities now employ automated air pressure chambers that seal the watch and subject it to a standardized 3 ATM test cycle. This automation ensures every unit undergoes the exact same stress profile, reducing the likelihood of false passes caused by operator haste. While this does not guarantee deep diving capability, it validates the integrity of the gasket seating and crystal seal under standard atmospheric pressure changes.
Where Humans Still Dominate
Despite these advancements, machines struggle with subjective aesthetic qualities and complex reflective surfaces. Dial printing quality and hand alignment remain primarily under human supervision. Optical sensors often fail to distinguish between acceptable ink variance and actual defects on textured dials. For models like the Navitimer, the complexity of the slide rule markings and the interplay of light on the bezel confuse automated vision systems. Human inspectors are still required to verify the symmetry of sub-dials and the luminous application under specific lighting angles that machines cannot replicate.
Expert Authentication Insight
Physical diagnostic: Check the case back engraving depth consistency. Laser automation creates uniform depth across all characters. If you feel significant depth variation between letters using a fingernail or loupe, the unit likely bypassed the new optical scanning line or belongs to an older batch produced before the 2026 upgrades.
The 20-Point Checklist: Leaked Inspection Sheet
Internal documents obtained from the assembly floor reveal a standardized 20-point inspection protocol enforced before boxing. This checklist is not marketing material; it is the operational baseline for QC technicians. While adherence varies by shift and workload, these twenty points represent the factory’s definition of a shippable product. Understanding this list allows buyers to replicate the factory’s inspection process upon receipt.
Case and Crystal Points (1-5)
The initial phase focuses on external integrity. Inspectors verify case scratches under high-lux lighting, ensuring no hairline marks exist on polished surfaces. Lug symmetry is checked visually and with digital calipers to ensure even spacing. Crystal dust is an automatic failure point; any particle visible under the glass results in immediate disassembly. AR coating integrity is examined for peeling or bubbles, particularly around the edges. Finally, case back engraving depth is measured to ensure it meets the minimum micron threshold for clarity and tactile feel.
Movement and Function Points (6-12)
Functional reliability is tested through a series of operational checks. Timekeeping rate is recorded on a timegrapher in multiple positions. Amplitude must exceed the minimum threshold to ensure power reserve stability. Beat error is adjusted to remain within acceptable limits to prevent ticking noise. Date change speed is observed during the midnight transition to ensure instant snap rather than slow creep. Date alignment within the window is verified for centering. Crown screw-down torque is tested to ensure proper sealing without stripping threads. For chronographs, chronograph reset is checked to ensure hands return precisely to zero without deviation.
Bracelet and Clasp Points (13-20)
The final segment addresses wearability and hardware. Link play is assessed to ensure the bracelet does not feel loose or rattling. Clasp snap strength must provide audible and tactile confirmation of locking. Engraving clarity on the clasp is inspected for sharpness. Brushing alignment must flow continuously across links without interruption. End link fitment is checked for gaps between the case and bracelet. Screw tightness is verified to prevent links from separating during wear. For leather straps, strap stitching is examined for loose threads. The process concludes with an overall cleanliness check to remove fingerprints and dust before packaging.
Expert Authentication Insight
Physical diagnostic: Focus on Point 10 (Date Alignment) and Point 18 (Screw Tightness). These are the most common failure points in post-shipment inspections. Use a screwdriver to gently test torque on case back screws; if they turn with minimal resistance, the factory torque specification was not met.
Failure Rates: What Gets Scrapped
Quality control is ultimately an economic equation. Factories balance the cost of scrap against the risk of dealer returns. In 2026, the goal is not zero defects, but rather managing defects within a profitable margin. Understanding what gets rejected versus what gets reworked provides insight into the actual quality floor of the market.
Movement Rejection Rates
Internal data suggests approximately 5-8% of movements are rejected during final assembly due to instability or rate deviation. While VS factory publicly claims a rejection rate of less than 3%, independent tracking of batch returns indicates the figure is closer to 6% for complex calibers. Movements that fail to maintain amplitude after a 24-hour rest period are pulled from the line. These units are either sent back to the movement supplier or cannibalized for parts, rarely making it into a finished watch.
Cosmetic Rework vs. Scrap
Full scrapping is reserved for catastrophic failures. Approximately 15% of units require rework, such as repolishing case sides or removing and resetting hands. Only about 2% are fully scrapped. According to Panerai super clone factory comparison data, factories prefer rework to maximize material ROI, as the cost of steel and machining outweighs the labor cost of correction. A watch with a minor scratch on the lug will be polished down rather than discarded, provided the case dimensions remain within tolerance after material removal.
The “B-Grade” Market Leakage
Units that fail QC but remain functional are sometimes sold as “B-Grade” via unofficial channels. These watches lack warranty support and often possess cosmetic flaws exceeding the 0.5mm tolerance for alignment or finishing. They enter the market at a discounted rate, typically through dealers who do not advertise the defect status. Buyers encountering prices significantly below market average should suspect these units, as they bypassed the final approval stage but were deemed safe to sell mechanically.
Expert Authentication Insight
Physical diagnostic: Inspect the rehaut engraving alignment. Misalignment here often indicates a reworked unit where the movement was cased multiple times, increasing the risk of dust intrusion. If the logo on the rehaut does not align perfectly with the minute track, the watch likely underwent cosmetic correction before shipping.
Dealer Intervention: The Second QC Layer
Factory QC is the first line of defense, but it is not the last. In 2026, the relationship between buyer and factory is mediated by dealers who operate their own inspection protocols. This second layer exists not out of altruism, but financial necessity. A returned unit costs the dealer double shipping fees and potential inventory depreciation. Consequently, the dealer’s QC is often more rigorous than the factory’s, focused on survivability during transit and immediate visual appeal upon unboxing.
The Dealer’s Incentive Structure
Dealers lose money on returns. They perform a secondary QC to catch factory misses. This adds 24-48 hours to shipping time but reduces return rates by 30%. For a high-volume dealer moving BLS or VS factory pieces, a 5% return rate can erase monthly margins. This economic pressure forces a stricter interpretation of tolerances. While a factory might pass a Navitimer with a minor bezel alignment issue because it falls within the 0.5mm tolerance, a dealer knows this is the first thing a customer checks. They will reject units that technically pass factory standards but fail customer expectation standards. This divergence creates a tiered market where dealer-selected units command a premium over direct factory stock.
Photo Verification Protocols
Dealers send 10-15 high-res photos. This is the buyer’s only window into the pre-shipment state. Refusal to send photos indicates skipped QC. In 2026, standard protocol for units priced over $500 USD includes macro shots of the date window, case back engraving, and clasp mechanism. For a Superocean Heritage, expect close-ups of the ceramic bezel insertion to check for gaps. Some dealers provide timegrapher screenshots showing amplitude and beat error. If a dealer claims to offer QC but sends only blurry wrist shots, they are bypassing the inspection phase to accelerate turnover. Legitimate verification requires static, well-lit images where dust particles are visible if present.
Cost of Additional QC
Some dealers charge $10-$20 for detailed timegrapher reports. In 2026, this is standard for units over $500 USD. Free QC often means a visual glance only. The fee covers the labor of unboxing, winding, regulating, and re-boxing the unit. For a Chronomat replica costing upwards of $700 USD (converted from doubled RMB reference prices), skipping this service is a false economy. The cost represents less than 3% of the total purchase price but provides data on whether the movement was regulated after casing. Factories often regulate movements before casing; the stress of assembly can shift the rate. Dealer QC catches this drift.
Expert Authentication Insight
Physical diagnostic: Compare the dealer’s QC photos with the factory’s stock photos. If the second hand position differs significantly, the watch was moved or rewound, indicating potential handling issues. Specifically, check the date wheel alignment in the photos. If the dealer’s photos show the date centered but the factory stock shows it high, the unit was likely swapped or reworked. Consistency in lighting color temperature between photos also validates that the inspection occurred in a controlled environment rather than a casual desk check.
Future Proofing: 2027 Standards Preview
The trajectory of replica manufacturing is moving toward automation and data-driven quality control. While 2026 relies heavily on human vision augmented by basic tools, 2027 promises a shift toward AI-assisted verification and material science improvements. These changes aim to reduce the variance that currently defines the hobby. For collectors, understanding this roadmap helps distinguish between marketing hype and genuine technological upgrades.
AI-Driven Defect Recognition
Pilot programs are testing AI cameras to identify dial printing errors faster than humans. Expect 99% detection rates on text alignment by late 2026. Human inspectors suffer from fatigue, leading to missed flaws after hour three of a shift. AI systems do not tire. They can detect kerning errors in the BREITLING logo or inconsistent lume application that the human eye glosses over. Early adoption is visible in Clean factory lines where dial printing consistency has tightened noticeably in recent batches. This technology will eventually make dial flaws rare, shifting the focus of QC to case finishing and movement performance.
Material Traceability
Factories are beginning to log steel batch numbers. This allows tracking of corrosion issues back to specific material suppliers, improving long-term durability. In the past, a batch of corrosive steel might ruin a factory’s reputation for months before the source was identified. With traceability, problematic materials are isolated quickly. For the buyer, this means better long-term wear resistance on bracelets and cases. BLS factory has hinted at implementing this for their bullet bracelet production, claiming their 904L steel sourcing is now fully documented. While unverifiable by the end user, the internal pressure to maintain batch consistency drives higher overall material standards.
The Push for Zero Dust
Clean rooms are upgrading to ISO Class 8 standards. The goal is to eliminate dust under the crystal entirely, a major pain point in 2025 models. Dust intrusion remains the most common cosmetic complaint in high-end replicas. It undermines the illusion of quality regardless of movement accuracy. New casing procedures involve positive pressure environments and ultrasonic cleaning steps prior to final assembly. While zero dust is an aspirational target, the reduction in visible particulate matter under the crystal is already measurable in 2026 production runs. Expect fewer units requiring case opening for cleaning upon arrival.
Expert Authentication Insight
Physical diagnostic: Keep an eye on the dial texture consistency. As AI inspection ramps up, expect flawless printing but potentially sterile perfection that lacks the microscopic texture of genuine hand-finishing. Under a 10x loupe, genuine dials often show slight irregularities in paint grain or printed index edges. AI-perfect dials may appear too uniform, lacking the depth of genuine manufacturing processes. This sterile perfection is itself a marker of replication in 2027. Look for the presence of natural variance in lume application; too much consistency suggests machine application without manual finishing.
Understanding factory QC standards does not guarantee a perfect watch; it guarantees you know what imperfections are negotiable. In 2026, the factory’s goal is yield, not perfection. Your goal as a buyer is to identify which of the 20 checklist points matter to your wrist and which are statistical noise. Do not pay a premium for perfect QC that does not exist. Pay for transparency in the failure points that do. When a dealer admits a bezel is off by 0.4mm but guarantees the movement is within +5 seconds/day, they are offering value. When they claim flawlessness, they are selling fiction. The mature collector buys the data, not the promise.